A shipment of sludge vacuum pumps manufactured by GN Separation & Conveying has been delivered to overseas customers, marking another export order for air-operated solids transfer equipment in the environmental and oilfield waste management sector.
The pumps are designed to handle high-solids, high-viscosity materials that conventional centrifugal or screw pumps struggle to transport efficiently. The core technology is a fully pneumatic vacuum pump that uses compressed air to create negative pressure, drawing slurry into the chamber and then discharging it through air pressure. This cycle repeats continuously, allowing for reliable transfer of materials that would otherwise clog or damage standard pumping equipment.
The decision to use air-operated vacuum pumps rather than electric or diesel-driven alternatives reflects specific operational requirements. In explosive or hazardous environments such as offshore platforms and oil and gas fields, the absence of electrical components eliminates ignition risks and simplifies compliance with safety regulations. The pumps also have no internal rotating parts, which reduces mechanical wear, prevents cavitation and dry-run damage, and lowers maintenance costs over the equipment’s service life.
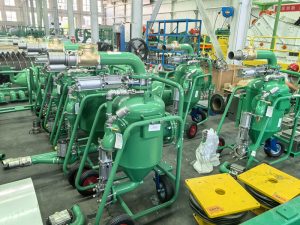
The shipped units are constructed from stainless steel and feature triple-sealing technology to prevent leakage during operation. This is particularly relevant for applications involving oily sludge, drilling cuttings, and chemical waste, where containment is both an environmental and safety concern. The pumps can handle solid particles up to 50 mm or 75 mm depending on the model, with solids content reaching as high as 80 percent in some slurry compositions.
Three standard capacity models are available: 10 cubic meters per hour, 20 cubic meters per hour, and 40 cubic meters per hour. Each model requires different air pressure and volume inputs, and customers typically source air compressors locally to reduce shipping costs and simplify maintenance. The pumps operate on a simple cycle: suction, discharge, and repeat, with adjustable timing to match specific material characteristics and project requirements.
The export order includes units destined for customers in Europe, the Middle East, and Asia. Previous deliveries of similar equipment have been used in tank bottom sludge removal, drilling waste transfer, mining tailings handling, and long-distance slurry transport between pits and rig sites. In several cases, customers reported that the vacuum pumps resolved persistent problems with blockages and excessive downtime that had plagued their previous pumping systems.
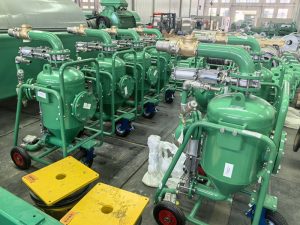
GN Separation & Conveying, based in Langfang near Beijing, has manufactured separation and conveying equipment for 13 years. The company operates three production facilities and maintains branch offices in Moscow and Houston to support international sales and service. Its product line includes centrifuges, disc separators, sludge vacuum pumps, oil-water separators, and screw conveyors. The company exports to markets including the United Kingdom, Norway, Greece, Portugal, Russia, Mexico, India, Malaysia, Nigeria, Mozambique, Mongolia, the United Arab Emirates, Oman, and Saudi Arabia.
For this particular shipment, the pumps were configured to meet the customer’s specifications for material composition, transfer distance, and discharge height. GN offers testing services where customers can send material samples to verify pump performance before finalizing equipment selection. This approach reduces the risk of mismatch between equipment capabilities and actual operating conditions.
The global market for sludge and solids transfer equipment continues to grow as environmental regulations tighten and industrial operators seek to reduce waste handling costs. Traditional methods of moving high-solids slurries often involve manual labor, expensive trucking, or complex conveyor systems that require significant infrastructure. Vacuum-based transfer offers a flexible alternative that can be deployed in remote locations, confined spaces, and hazardous areas without extensive site preparation.
Air-operated vacuum pumps also align with broader trends in industrial equipment design: fewer moving parts, lower energy consumption, and simplified maintenance. Since the pumps do not require priming and can run dry without damage, they are less vulnerable to operator error and unexpected process upsets. The absence of electrical motors also means the equipment can operate in areas without reliable power supply, which is common in oilfields, mining sites, and temporary waste treatment facilities.
The shipment reflects the ongoing internationalization of Chinese industrial equipment manufacturers. Companies like GN Separation & Conveying compete not only on price but also on technical capability, customization, and after-sales support. Export orders to established markets in Europe and the Middle East indicate that these manufacturers have met the quality and reliability standards required by international customers.
For the receiving customers, the vacuum pumps are expected to improve waste handling efficiency, reduce labor requirements, and lower long-term maintenance costs compared to alternative pumping technologies. The equipment will be integrated into existing waste management systems, where it will transfer sludge from collection points to storage tanks, processing units, or disposal sites.
GN Separation & Conveying continues to accept orders for sludge vacuum pumps in various configurations and capacities. The company provides technical consultation to help customers select the appropriate model based on material properties, transfer distance, and site conditions.